PHONE: (847) 253-6000
TOLL FREE: (800) 52-MOTOR
Explore our export-grade range of high-efficiency brushless DC motors, precision helical gearheads, harmonic actuators, and specialized EV drive components engineered for medium to high-volume OEM programs.
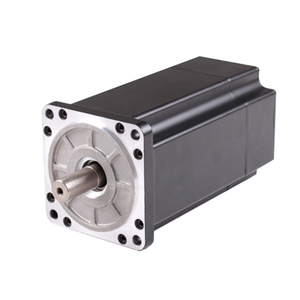
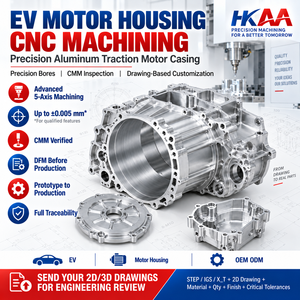
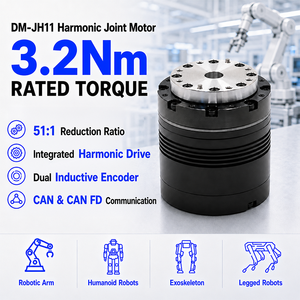
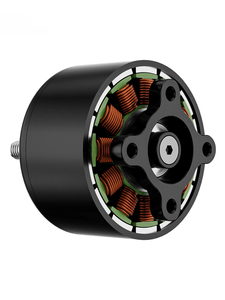
In high-duty industrial automation, commercial refrigeration, medical pumps, and robotics, the choice of electro-mechanical drive architecture directly dictates system efficiency, noise, vibration, and total cost of ownership (TCO). As a premier wholesale manufacturer and exporter in China, our operations integrate decades of legacy motor engineering—originally pioneered by American fractional horsepower (FHP) manufacturing standards—with modern precision CNC gear machining and micro-geometry tooth profiling.
The helical gear design operates on an inclined tooth helix angle, typically engineered between 15° and 30°. This oblique tooth layout increases the contact ratio significantly compared to straight spur gearing. The continuous contact line reduces contact stress ($\sigma_H$) and bending stress ($\sigma_F$), preventing premature surface fatigue, pitting, and tooth spalling under high start-up torque or continuous reversing cycles.
Our manufacturing facilities utilize high-precision hobbing and grinding machinery capable of achieving ISO 1328-1 Grade 5 gear accuracy. Combined with 20CrMnTi low-alloy steel carburizing and case hardening to HRC 58-62, our helical gear sets handle maximum overhung loads (OHL) without compromising gear mesh positioning or inducing gear deflection.
Multiple teeth engage simultaneously, spreading the load evenly to withstand sudden torsional overload spikes up to 300% of nominal torque.
Micro-crowning tooth profiles minimize gear mesh impact noise, satisfying stringent indoor commercial appliance and medical equipment standards.
Precision die-cast aluminum housing housings optimize thermal flux paths, maintaining internal lubricant viscosity over 20,000 continuous hours.
Selecting the appropriate drive architecture requires evaluating key operational parameters including torque density, backlash, acoustic output, and efficiency. Below is an engineering comparison matrix for OEM specifiers:
| Platform Technology | Stage Mechanical Efficiency | Acoustic Output (dBA) | Backlash Tolerance | Ideal OEM Application Envelopes |
|---|---|---|---|---|
| Helical Parallel Shaft | 95% – 98% | < 45 dB | 15 – 30 arcmin | Continuous duty pumps, ice makers, HVAC dampers, food service |
| Planetary Gearbox | 90% – 95% | 55 – 65 dB | 3 – 10 arcmin | High-density robotics, servo positioning, heavy-duty AGVs |
| Right-Angle Worm Gear | 55% – 82% | 50 – 58 dB | 30 – 60 arcmin | Self-locking conveyors, low-cost right-angle drives |
| Harmonic Joint Drive | 75% – 88% | < 50 dB | < 1 arcmin (Zero Backlash) | Humanoid AI joints, surgical robots, aerospace gantry systems |
| Brushless DC Direct Drive | 88% – 94% | < 38 dB | 0 arcmin | High-speed fans, traction hubs, lightweight UAV propellers |
The global motion control market is undergoing a rapid transition toward energy-efficient, smart, and ultra-compact drive systems. OEM procurement managers sourcing from China must align their supply chain strategies with these critical technical shifts:
Legacy AC shaded-pole and Permanent Split Capacitor (PSC) motors are rapidly giving way to BLDC and PMSM drive units. By pairing high-efficiency helical gearheads with electronically commutated motors, engineers achieve precise speed regulation across variable frequency bands, reduced heat dissipation, and compliance with stringent IE4 and IE5 global energy efficiency regulations.
Modern factory automation and mobile robotic platforms require direct communication between gearmotors and central PLC network nodes. Future-ready gearmotors are supplied with integrated dual inductive encoders, hall sensors, and native support for CANopen, EtherCAT, and Modbus RTU communications protocols. This enables real-time predictive maintenance telemetry, tracking temperature rise, vibration signatures, and load torque profiles.
Overseas buyers demand shortened product development cycles. Utilizing standardized modular gear housings, motor flanges, and interchangeable shaft options (hollow, solid, keyway, or D-cut), suppliers can quickly configure custom winding voltages, stack lengths, and gear ratios without incurring expensive tooling delays.
To maintain a competitive edge, our research and engineering teams focus on advanced material science and automated quality validation workflows:
Inheriting over six decades of American fractional horsepower motor design heritage, our manufacturing facility operates under strict international quality frameworks. We don't just supply standard off-the-shelf items—we build tailored, application-specific motion solutions engineered to your exacting tolerance profiles.
Our state-of-the-art facility encompasses all core manufacturing stages under one roof to ensure complete traceability and rapid engineering change management:
A fractional horsepower gearmotor delivers output power under 1 horsepower (746 Watts). It pairs a high-speed electrical motor (AC, PMDC, or BLDC) with an integrated helical gear reduction train. The gearhead trades high rotational motor speed for elevated output torque at lower RPM, allowing compact machinery—such as augers, pumps, dampers, and conveyors—to operate reliably under continuous loads.
Helical gearmotors feature teeth cut at an angle to the gear axis. This results in progressive tooth engagement, yielding higher contact ratios, greater torque capacity, superior shock load resistance, and substantially quieter operation compared to straight-cut spur gears, which experience cyclic impact noise during mesh engagement.
Our engineering team modifies magnetic circuit windings (wire gauge, turns, voltage ratings), gear ratios (single to multi-stage reductions), output shaft geometries (D-cut, dual flat, splined, hollow-bore), mounting flange profiles, thermal cutout switches, and connector wire harnesses based on your specific application duty cycle and torque targets.
We maintain ISO 9001:2015 and ISO 13485:2016 quality management systems. Every product lot undergoes incoming material inspection (IQC), in-process winding/gear mesh monitoring (IPQC), 100% end-of-line electrical, acoustic, and torque dynamometer testing (FQC), and life-cycle verification under thermal overload conditions.
Custom engineering sample prototypes are typically delivered within 2 to 3 weeks following specification sign-off. Mass production volume releases generally range between 4 to 6 weeks, supported by flexible air or sea freight logistics options from major ocean ports in China.
Yes. We manufacture low-voltage permanent magnet DC (PMDC) and Brushless DC (BLDC) helical gearmotors optimized for 12V, 24V, 48V, and 72V DC battery power rails, delivering maximum efficiency to preserve energy in off-grid, agricultural, or mobile EV platforms.
Need custom gear ratios, engineering sample evaluation, or wholesale pricing for your high-volume OEM program? Our technical engineering team is ready to analyze your application requirements.
Get a Quote