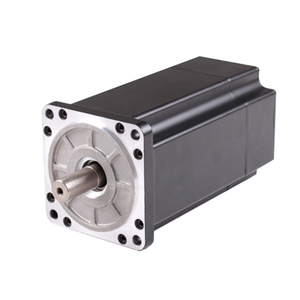
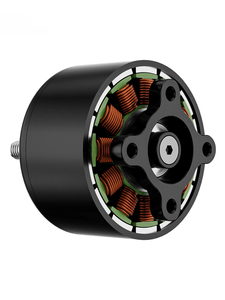
High Speed 3 Phase 48v 310v 3000rpm 1kw 1.5kw 2kw 3kw 110mm Nema 42 Brushless DC Motor for Robot
Explore our specialized portfolio of sub-fractional to high-power brushless DC motors, precision planetary speed reducers, custom housings, and heavy-duty drivetrain kits. Built to withstand demanding OEM operating environments with maximum power density and high torsional stiffness.
In high-performance industrial motion control, the selection of a Custom OEM Planetary Gearbox represents a pivotal engineering decision. Unlike conventional parallel shaft or right-angle worm gear units, planetary gear trains distribute mechanical load across multiple planet gears simultaneously. This co-axial geometry provides an extraordinary power density, minimizing radial journal stresses and maximizing torque throughput in constrained mechanical footprints.
Modern planetary reducers consist of three primary co-axial components: a central sun gear driven by the prime mover (such as a high-speed Brushless DC or Stepper motor), multiple floating planet gears mounted on a rigid planetary carrier, and an internal tooth ring gear (annulus) integrated directly into the outer structural housing. By dividing the total shaft load equally across 3, 4, or 5 planet gears, pitch line velocities are normalized, and gear tooth deflection is minimized under peak transient impact conditions.
To achieve high positional repeatability in servo-driven robotics, medical diagnostic equipment, and automated guided vehicles (AGVs), custom OEM factories focus on three primary mechanical factors:
Utilizing dual-supported planet carriers machined from single-piece forged steel or aviation-grade 7075 aluminum to eliminate cantilever flexing during reversal loads.
Implementing helical gear tooth profiles polished with AGMA Class 12 precision grinding, optimizing contact ratios to reduce acoustic signature below 55 dBA.
Precision-matched planet gear sets categorized into sub-micron tolerance bands, achieving standardized backlash down to <1 arcmin for surgical and optical tracking applications.
When selecting a gear reducer factory, engineering teams must look beyond standard catalog torque ratings. The true performance envelope depends on continuous operational duty cycle ($S1$ vs $S5$ indexing duty), thermal dissipation characteristics of the housing, gear tooth bending fatigue strength (evaluated via AGMA/ISO 6336 standards), and bearing L10h life calculations under combined axial and radial overhung loads.
The table below provides detailed engineering metrics across various planetary gearbox architecture configurations manufactured in OEM facilities for high-volume programs.
| Gearbox Platform Series | Gear Ratio Range | Efficiency Rating (%) | Standard Backlash (arcmin) | Precision Backlash (arcmin) | Housing Material Spec | Primary OEM Target Sector |
|---|---|---|---|---|---|---|
| PG-Micro (NEMA 11-17) | 3:1 to 512:1 | 88% - 94% | ≤ 12 | ≤ 5 | AL 6061-T6 / Anodized | Medical Dosing & Surgical Robotics |
| PG-Servo (NEMA 23-42) | 3:1 to 100:1 | 92% - 97% | ≤ 7 | ≤ 3 | 20CrMnTi Alloy Steel Case Hardened | CNC Automation & Industrial Arms |
| PG-Heavy Duty (EV/AGV) | 4:1 to 200:1 | 90% - 95% | ≤ 9 | ≤ 4 | Ductile Iron QT500-7 / Carburized Steel | Forklifts, Excavators & Traction Drives |
| PG-Right Angle Planetary | 3:1 to 150:1 | 85% - 92% | ≤ 10 | ≤ 6 | Cast Aluminum / High-Stiffness Steel | Conveyors, Packaging & Restricted Space |
| PG-Synchronous Medical | 5:1 to 64:1 | 94% - 96% | ≤ 5 | ≤ 1 | Stainless Steel 316L / ISO 13485 Spec | Infusion Pumps, Scanners & Diagnostics |
As an industry leader operating inside a rich American gear-building legacy since 1954, our manufacturing infrastructure combines six decades of mechanical gear engineering with computerized quality validation systems. Rooted in the engineering traditions established by Molon Motor & Coil Corporation in Arlington Heights and Rolling Meadows, Illinois, our customized planetary production lines exemplify modern advanced manufacturing.
True OEM performance is not achieved by chance; it is governed by rigorous regulatory quality management systems. Our operations maintain direct compliance with ISO 9001:2015 for industrial component manufacturing and ISO 13485:2016 for medical device component integration, complemented by UL recognized component listings across demanding motor-gear combinations.
Every gear raw bar batch undergoes optical emission spectrometry to verify chromium, molybdenum, and nickel alloy concentration, followed by vacuum carburizing to achieve surface hardness of 58-62 HRC while maintaining a tough core structure.
Our factory floor features 6-axis Swiss CNC hobbing and hard gear grinding centers capable of achieving tooth pitch errors within ±0.001mm, eliminating acoustic vibration and parasitic thermal losses.
100% of custom assembled planetary gearboxes pass through automated test benches measuring no-load current, running torque, thermal rise, backlash in both rotation directions, and FFT vibration spectrum analysis.
Off-the-shelf speed reducers frequently force system integrators to compromise on mounting space, input shaft fitment, or thermal ratings. Our custom OEM engineering process eliminates these compromises through a structured co-development workflow:
Our application engineers analyze your continuous torque ($T_2$), peak acceleration torque ($T_{2B}$), emergency stop torque ($T_{2NOT}$), input speed range ($n_1$), expected radial load ($F_{rx}$), and axial thrust forces ($F_{ax}$).
Selection of single-stage (3:1 to 10:1), dual-stage (12:1 to 100:1), or triple-stage (100:1+ ratios). Gear micro-geometry is optimized for spur or helical tooth engagement depending on noise constraints.
Specification of synthetic polyglycol or polyalphaolefin (PAO) greases customized for operating environments ranging from arctic low temperatures (-40°C) to high-temperature food processing (+120°C with NSF-H1 registration).
Customizing motor mounting adapter plates, input clamping collars, output shaft keyed geometry, hollow shaft splines, or D-cut profiles for zero-slip torque transmission.
As global automation transitions toward higher energy efficiency, autonomous mobility, and artificial intelligence integration, the demand on custom OEM planetary gear factories is shifting rapidly. Key technological and procurement trends transforming planetary gearbox design include:
In electric vehicle (EV) traction, commercial utility equipment, and battery-powered agricultural crawlers, engineers require planetary gearboxes capable of accepting input motor speeds exceeding 12,000 RPM. These high input speeds demand advanced lubrication dynamics, low-friction lip seals, and dynamic balancing of sun gear input couplings to prevent thermal runaway.
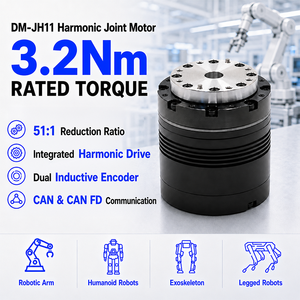
Robotic joint actuators in next-generation humanoid AI applications require ultra-compact form factors with zero back-drive backlash. OEM factories are increasingly producing hybrid actuators combining dual-stage planetary stages with harmonic strain-wave elements, integrating embedded magnetic encoders and CAN-FD communication buses directly into the gearbox housing structure.
Modern industrial gearboxes are evolving into active sensor nodes. High-tier OEM planetary factories now integrate micro-vibration piezoceramic sensors and real-time RTD thermistors inside the ring gear housing. This allows real-time condition monitoring, calculating grease degradation and gear tooth wear before critical equipment downtime occurs.
With global supply chains prioritizing carbon reduction, custom OEM factories are adopting powder metallurgy (PM) sintering for non-structural planet gears and utilizing high-tensile magnesium-aluminum alloys for structural casings. This achieves up to 35% mass reduction without compromising torsional fatigue resistance.
Procuring custom planetary speed reducers for high-volume manufacturing programs entails significant risk management. A failure in gear heat treatment or tooth grinding tolerances can result in catastrophic field recalls. When evaluating potential planetary gearbox factories, procurement directors should audit four crucial operational indicators:
Ensure the facility performs critical gear hobbing, heat treatment, housing machining, and pin grinding internally rather than relying 100% on unverified sub-tier vendors.
Verify valid ISO 9001:2015 and ISO 13485:2016 certificates issued by accredited registrars, along with documented PPAP (Production Part Approval Process) Level 3 compliance.
Look beyond initial piece-part prices. Factor in gear efficiency gains (reducing battery consumption in mobile systems), lower field warranty claim rates, and component longevity.
Connect directly with our engineering team in Arlington Heights, Illinois to discuss gear ratios, load calculations, custom shaft envelopes, and high-volume factory production schedules.