PHONE: (847) 253-6000
TOLL FREE: (800) 52-MOTOR
Explore our premier line of pneumatic drives, high-torque brushless gearmotors, custom motor housings, and industrial motion solutions built for critical operating environments.
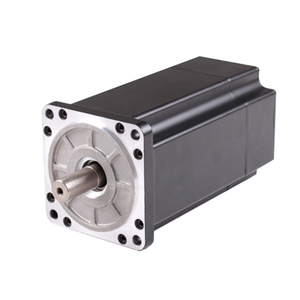
Engineered for heavy-duty robotics and automated industrial positioning. Features high thermal tolerance, 3000 RPM continuous output, and multi-voltage flexibility (48V to 310V DC).
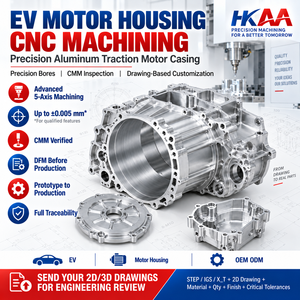
ISO 9001 certified lightweight aluminum alloy casings designed for pneumatic actuators and electric vehicle traction drives. Delivers optimal heat dissipation and structural strength.
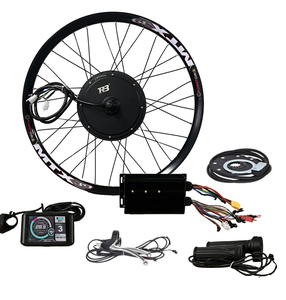
Heavy-duty direct-drive motor assembly tailored for rugged utility vehicles, mobile material handling equipment, and custom OEM high-load platform drive systems.
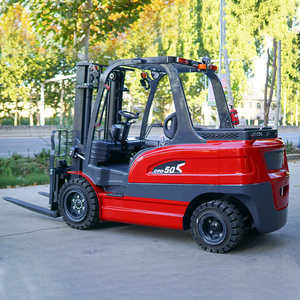
Designed for narrow-aisle warehouse operations. Accommodates 2 Ton to 5 Ton load capacities with explosion-proof safety options for hazardous chemical logistics.
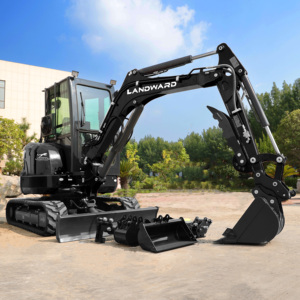
Rugged 1 Ton to 3.5 Ton mini track power units certified to EPA/CE standards. Optimized for high overhung radial loads and harsh field operating environments.
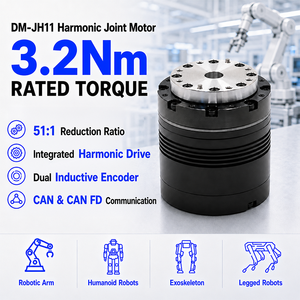
Dual inductive encoder robotic joint drive providing sub-arcminute angular precision. Ideal for precision automated assembly arms and intelligent industrial robotics.
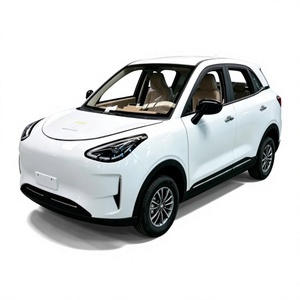
High-torque continuous duty motor engineered for off-highway vehicles and industrial site transportation, maximizing range and battery duty cycles.
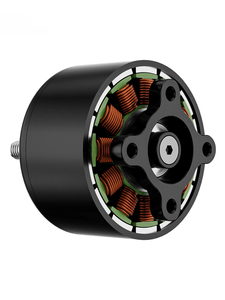
Lightweight high-speed dynamic rotor motor engineered for aerial surveillance, industrial inspection UAVs, and high-frequency automated payload delivery.
As a global leader in fractional horsepower (FHP) motion solutions, pneumatic air motors, and precision gear drives, our manufacturing operation brings together state-of-the-art engineering, certified quality frameworks, and deep application experience. While electric motors dominate general automation, industrial pneumatic motors remain the gold standard for ATEX-regulated explosion-proof environments, high-moisture processing zones, continuously stalled tensioning systems, and intense electromagnetic interference (EMI) conditions.
Rotary vane pneumatic motors deliver instant acceleration, high power-to-weight ratios, and reliable operation across a broad RPM spectrum (from 300 RPM up to 10,000 RPM). Utilizing compressed air expanding against sliding vanes housed inside an eccentric rotor chamber, these motors generate continuous torque with zero thermal buildup during prolonged stall conditions.
For applications demanding high starting torque, low speed control, and heavy overhung load limits, radial piston pneumatic motors deliver maximum mechanical efficiency. Driven by reciprocating pistons pushing against a central crankshaft, these drives maintain robust output under heavy duty cycles without requiring complex gear reductions.
System designers and OEM procurement directors must evaluate thermal performance, hazardous atmosphere compliance, total cost of ownership (TCO), and duty cycle resiliency when selecting primary movers. The table below illustrates core performance parameters verified through rigorous lab testing and field telemetry.
| Drive Technology | Power-to-Weight Ratio | Explosion Safety (ATEX) | Stall Resistance | Thermal Overheat Risk | Ideal Industrial Application |
|---|---|---|---|---|---|
| Vane Pneumatic Motor | Very High (up to 2 kW/kg) | Intrinsic / Ex II 2 GD c T4 | Indefinite (No damage) | Zero (Cooling air expansion) | Mixing tanks, paint sprayers, chemical pumps, mining hoists |
| Piston Air Motor | High (High low-speed torque) | Intrinsic / Ex II 2 GD c T4 | Indefinite (No damage) | Zero (Cooling air expansion) | Winches, offshore rigs, heavy conveyors, pipe crawlers |
| Brushless DC Motor (BLDC) | High | Requires Purged Enclosure | Thermal cutoff needed | Moderate to High | Robotics, EV drives, automated AGV platforms, UAV inspection |
| AC Induction Motor (PSC) | Moderate | Heavy Explosion-Proof Frame | High risk of winding failure | High if cooling fan stops | HVAC blowers, commercial refrigeration, food service machinery |
| Hybrid Stepper Motor | Moderate | Not recommended for hazardous zones | Stalls without damage, loses position | Moderate | Precision dosing pumps, lab diagnostics, automated valves |
Operating out of vertically integrated, ISO-certified manufacturing plants, our engineering team manages every critical phase of motor production in-house: high-speed CNC metal machining (maintaining micro-level tolerances of ±0.01mm), automatic stator coil winding, high-precision gear train cutting, dynamic rotor balancing, and complete cleanroom assembly for medical and critical industrial grade components.
Our Quality Management System (QMS) maintains strict compliance with ISO 9001:2015 industrial standards and ISO 13485:2016 medical device component standards. Full material batch traceability, rigorous dimensional CMM inspection, and documented failure mode effects analyses (FMEA) back every production batch released from our facility.
Before shipment, 100% of finished pneumatic motors, gearmotors, and custom electric drives undergo dynamic load testing. Torque-speed curves, stall force limits, air consumption (SCFM / m³/min), acoustic noise emissions, and shaft vibration profiles are captured digitally to guarantee compliance with client engineering specifications.
Global supply chain managers, OEM procurement directors, and industrial plant engineers face evolving regulatory, environmental, and technological landscapes. As heavy industry transitions toward smarter, cleaner, and more energy-efficient automation, four macro procurement trends are shaping the future of pneumatic motor sourcing:
Traditional pneumatic motors require lubricated air lines to prevent vane wear and cylinder scoring. However, food processing, pharmaceutical packaging, cleanroom manufacturing, and environmental sampling demand zero-oil exhaust emissions. Sourcing strategies are rapidly prioritizing air motors constructed with self-lubricating synthetic vanes (such as glass-filled PEEK or fluoropolymer matrices), ceramic bearings, and corrosion-resistant stainless steel housings.
Compressed air represents one of the highest energy costs in industrial manufacturing. Modern B2B buyers no longer evaluate pneumatic air motors solely on initial purchase price; energy consumption over the product lifecycle dominates TCO metrics. Procurement teams are specifying integrated smart electro-pneumatic valves and digital flow meters that dynamically throttle air volume during low-load intervals.
While pneumatic motors excel in explosive atmospheres and raw torque generation, electrical systems excel in precise multi-axis positioning. Modern automation architects are increasingly procuring hybrid motion architectures where compact pneumatic motors provide high-force power backup or primary movement, paired with digital sensors and CAN bus/EtherCAT electronic feedback networks.
Off-the-shelf industrial catalog motors often require costly shaft adaptations, mounting brackets, or port modifications during machine integration. Modern enterprise buyers are actively consolidating vendors in favor of OEM/ODM suppliers who offer rapid engineering prototyping, custom gear ratio modifications, non-standard mounting flanges, and guaranteed global spare parts logistics.
To stay ahead of global competition, the next generation of industrial pneumatic motors incorporates cutting-edge material science, fluid dynamics modeling, and noise-dampening acoustic technology. Below are key technological breakthroughs driving modern pneumatic motor design:
Legacy air motors suffered from internal turbulence, pressure drops, and inefficient air expansion. By leveraging advanced 3D CFD simulation tools, engineers optimize the internal geometry of inlet and exhaust ports, maximizing kinetic energy transfer from compressed air to the rotor. This yields up to 18% higher mechanical efficiency compared to conventional rotary vane designs.
High exhaust noise has historically been a drawback of industrial air motors. Modern high-performance pneumatic motors integrate multi-chamber reactive mufflers and sound-absorbing porous sintered bronze or synthetic diffusers. These designs bring operating sound levels below 75 dBA without inducing restrictive backpressure that compromises output torque.
Industrial pneumatic motors frequently operate in harsh marine offshore environments, chemical washdown facilities, or high-humidity underground mines. Current material advancements include nickel-Teflon plating, hard anodized aluminum bodies, 316L stainless steel shafting, and specialized thermal spray ceramic coatings that withstand acidic, alkaline, and saline exposure.
To deliver massive rotational torque within space-constrained machine frames, air motor manufacturers are integrating high-efficiency planetary gearheads and hardened steel right-angle bevel gears directly into the motor housing. Compact modular gear trains allow output torque ratings exceeding 1,500 Nm while keeping total drive footprint minimal.
Proper sizing of a pneumatic motor requires calculating required speed, load torque, operating air pressure (bar or PSI), and total air volume consumption (SCFM or L/min). Unlike electric motors which maintain constant speed regardless of load until thermal trip, pneumatic motors operate on a dynamic torque-speed curve where maximum power output occurs at approximately 50% of free (unloaded) speed.
When selecting a pneumatic motor for continuous-duty industrial applications:
Whether you require standard explosion-proof air motors, custom planetary gearheads, high-precision CNC motor housings, or specialized OEM drive development, our technical team is ready to support your engineering requirements.